

Blog
How to Choose a Hydraulic Ironworker: Capacity, Throat Depth and Operators

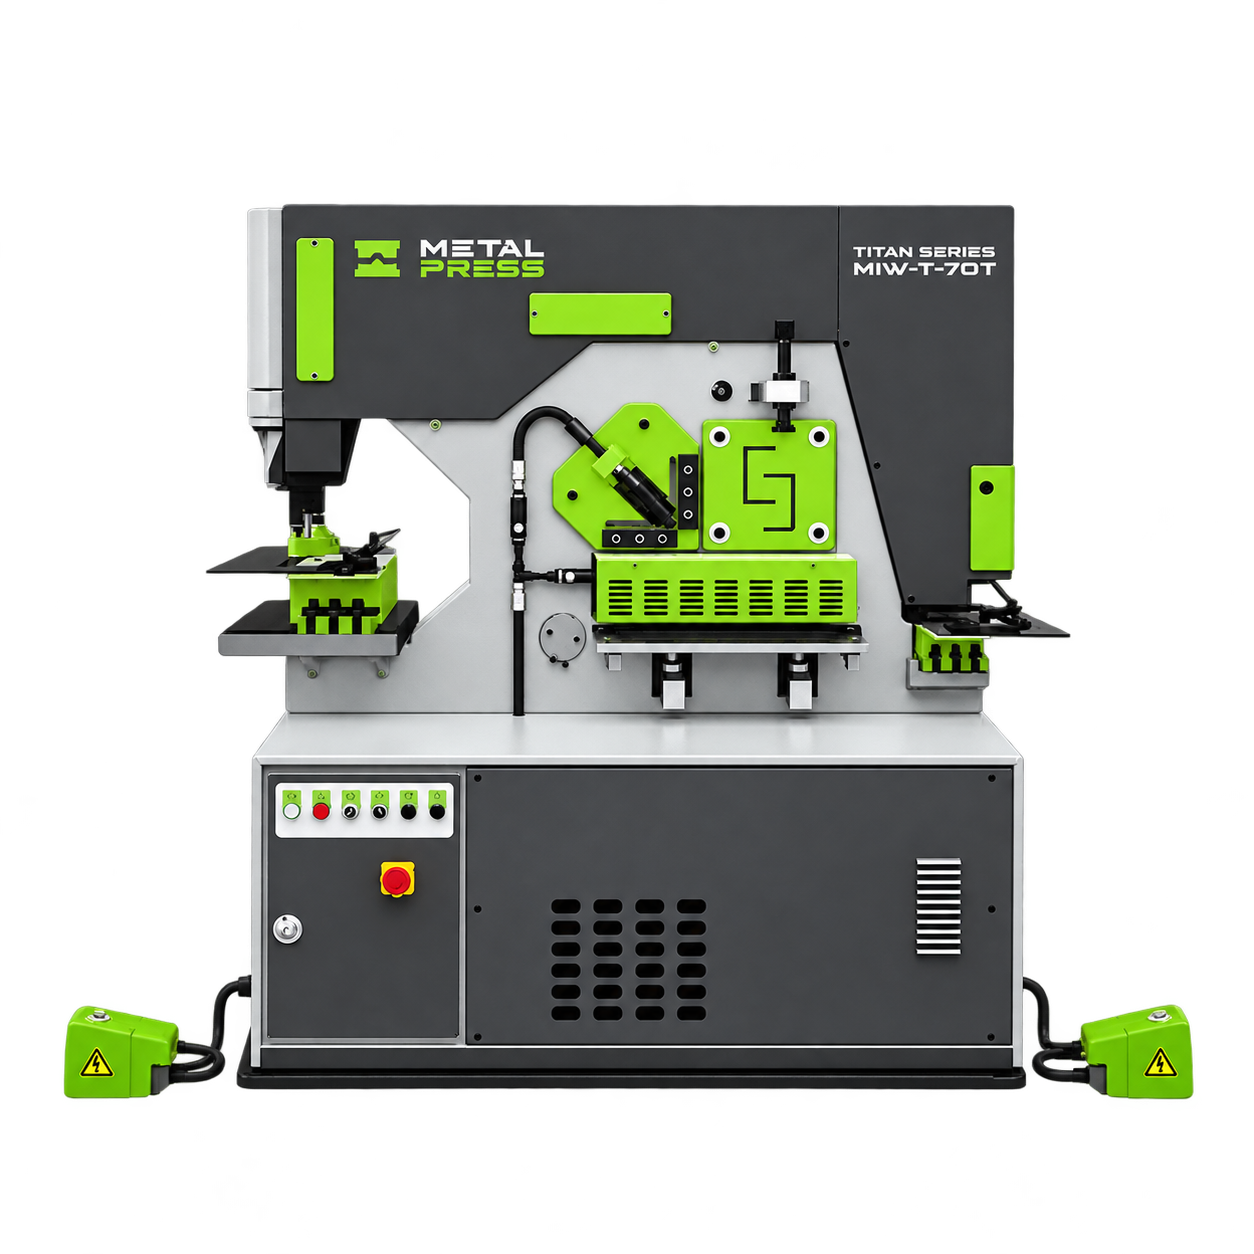
Choose a hydraulic ironworker by comparing every required workstation with the actual stock and feature geometry. Punching force, hole size, throat reach, section capacities, tooling and operator arrangement must all fit the job; one tonnage figure cannot describe the whole machine.
Make a workstation requirement list
Divide the work into punching, flat-bar or plate shearing, bar shearing, angle shearing and notching. For each operation, record material, dimensions, finished feature, quantities and positioning requirements. This prevents a machine with ample punching force from being selected for a section that does not fit another station.
The MIW-T hydraulic ironworker has separate station data and optional tooling information. Use those individual ratings rather than assuming that the largest plate thickness applies to every width or operation.
Understand punching force and hole requirements
Punching demand changes with the cut perimeter, thickness and material properties. A larger shaped hole can need a different tool and force review from a smaller round hole. Also check the tool supplier’s limits for the hole-to-thickness relationship, tool dimensions and material.
A die block that accommodates a certain die size does not establish the ability to punch that hole through the machine’s maximum listed plate thickness. Match the hole and material combination to the approved tool and machine documentation.
Selection checklist
| Requirement | Review separately | Common selection mistake |
|---|---|---|
| Punching | Hole, material, thickness and tool | Choosing from punch tonnage alone |
| Flat stock | Width and thickness combination | Using one maximum thickness everywhere |
| Angle and bar | Section dimensions and blade arrangement | Assuming every profile is standard |
| Notching | Profile, depth and access | Ignoring tool interference |
| Operator layout | Documented control and access arrangement | Assuming dual-operator means simultaneous cycles |
Check throat depth on the drawing
Throat depth affects how far a feature can be reached from an accessible edge. Mark every hole center and note which edge will enter the throat. Existing bends, angle legs and neighboring features can obstruct a setup even when the center distance appears to fit.
For repeat patterns, define the locating references, stops and support arrangement. See plate and angle punching and notching for feature-level planning and bracket fabrication for the complete component route.
MIW-T Hydraulic Ironworker
Compare individual workstation ratings, throat access, models and optional tooling.
Compare single- and dual-operator layouts carefully
Operator arrangement should follow the proposed work schedule and the machine’s documented control architecture. Ask how stations are accessed, which movements can be enabled and what restrictions apply when people work around different sides of the equipment.
The MIW-T is described as dual-operator. That label alone is not proof of simultaneous, independent punching and shearing cycles. Request confirmation of the specific operating arrangement instead of importing a competitor’s capability into the quotation.
Review tooling, support and repeat jobs
List round and shaped punches, dies, notch tools and any optional bending or structural tooling separately. Include how long stock is supported and how small parts are positioned and removed. Suitable stops and work tables matter to repeatability as well as machine force.
For a proposed batch of angle brackets, confirm stock cuts, hole reach and notch access before choosing the model. Add the material specification, drawings, quantities and available floor space to the enquiry. Ask the quote to distinguish the machine from separately supplied tooling and services.
Continue planning your fabrication workflow
Frequently Asked Questions
How much ironworker tonnage do I need?
Use the actual punching features and material data, then check every other required station independently. The machine and tooling documentation determine the approved combination.
Can throat depth limit a machine with enough force?
Yes. The workpiece must physically reach and locate at the tool. Check the accessible edge, angle legs and existing features.
Are all ironworker attachments included?
No. Confirm the supplied tooling and options in the quotation. The MIW-T page states that punches and dies are sold separately.
Discuss the actual part and equipment configuration
Send the drawing, material specification, quantities and acceptance requirements to MetalPress Machinery. Confirm the final machine, tooling and operating requirements against the supplied documentation and application review.
Further technical reading: Piranha: material-specific punch and die clearance review.