

Blog
What Is an Ironworker Machine? Five Fabrication Operations Explained

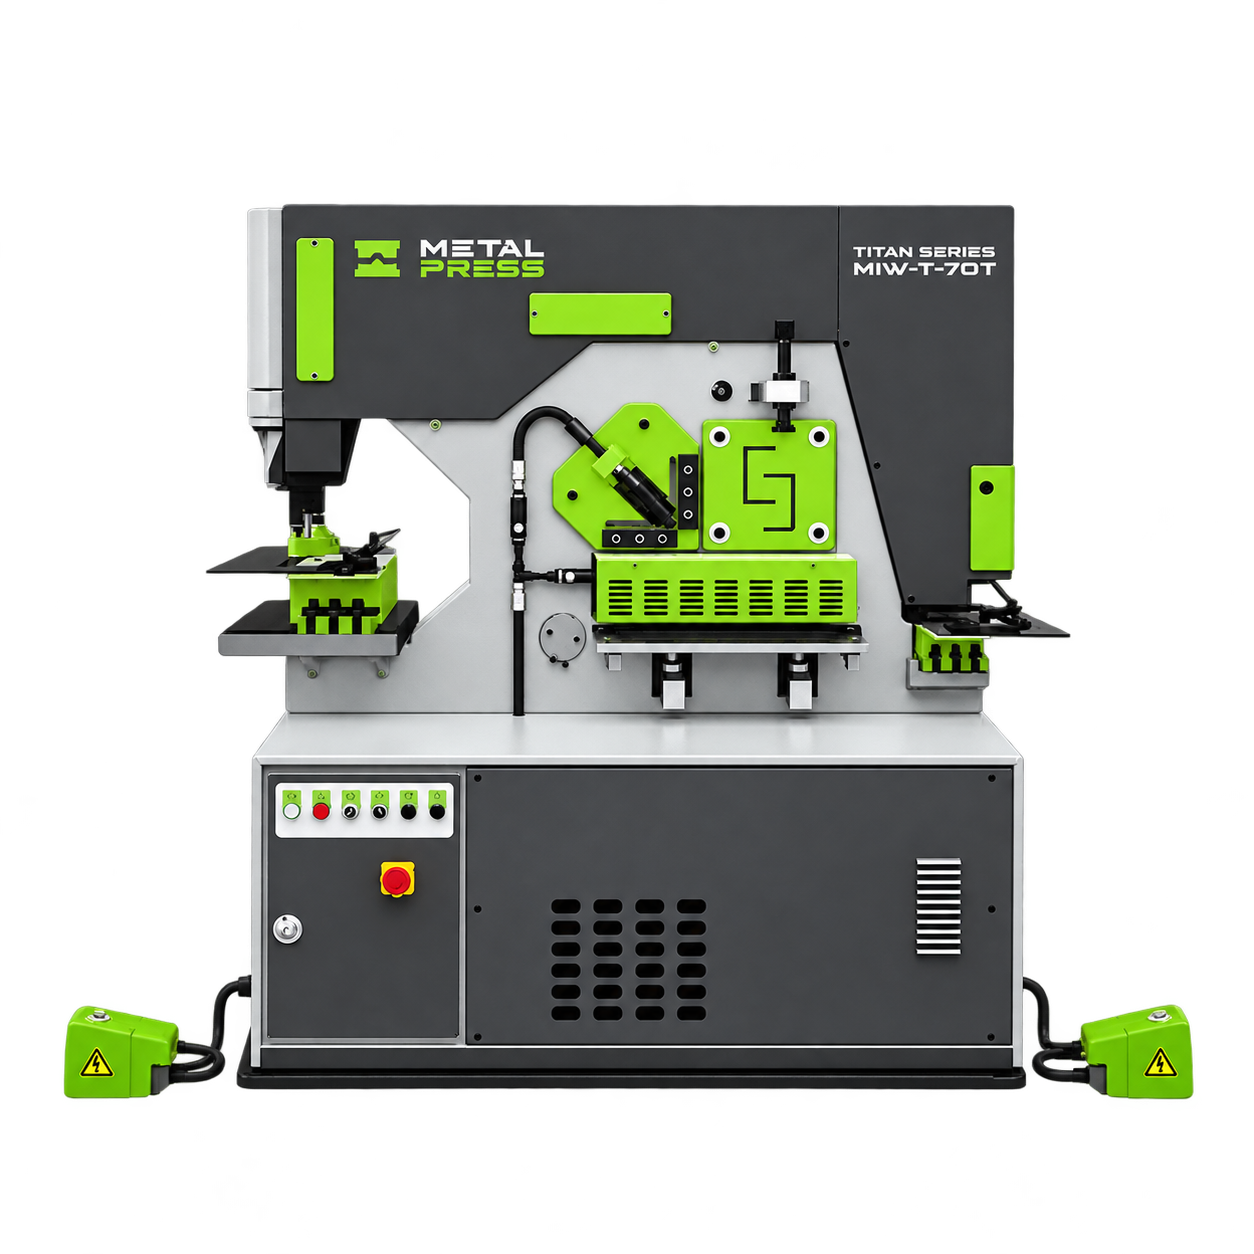
An ironworker machine combines dedicated metal-fabrication workstations such as punching, stock shearing and notching in one platform. It is equipment, not the ironworker trade or occupation. Its value is the ability to route suitable plate, bar and angle work through several operations, with each station selected by its own rating and tooling.
Punching makes holes with matched tools
The punching station uses a compatible punch and die to produce a specified feature in supported material. Hole shape, cut perimeter, material and thickness determine the application review. Tool reach and locating access matter alongside available force.
The largest tool that fits a holder is not automatically usable through the thickest plate rating. Review the actual hole and material combination, including tooling restrictions and the method used to position repeated features.
Flat-bar and plate shearing prepare straight stock
A flat-stock station cuts suitable material within a width-and-thickness combination. Check both dimensions in the station table rather than reading only the largest thickness. Some angle or miter arrangements require specific blades and positioning.
For long stock, include support on the entry and cut-piece sides. A workstation designed for local bar or plate cuts does not automatically replace a long-bed guillotine shear for full-width sheet blanks.
Selection checklist
| Workstation | Typical planning input | Capacity check |
|---|---|---|
| Punching | Hole shape, location and material | Tool and force limits plus throat access |
| Flat stock | Width, thickness and cut angle | Permitted dimension combination |
| Round/square bar | Section size and grade | Correct blade/section rating |
| Angle shearing | Leg dimensions and thickness | Applicable station and cut geometry |
| Notching | Profile, depth and location | Tool envelope and material limit |
Bar and angle shearing use section-specific arrangements
Round bars, square bars and angles have different contact and blade requirements. State the section dimensions, material and desired end geometry. Confirm whether the exact profile fits a standard station or needs an optional attachment.
See angle iron and flat-bar fabrication for a stock-preparation workflow. Do not infer channel cutting, beam coping or every miter angle from the general word ironworker.
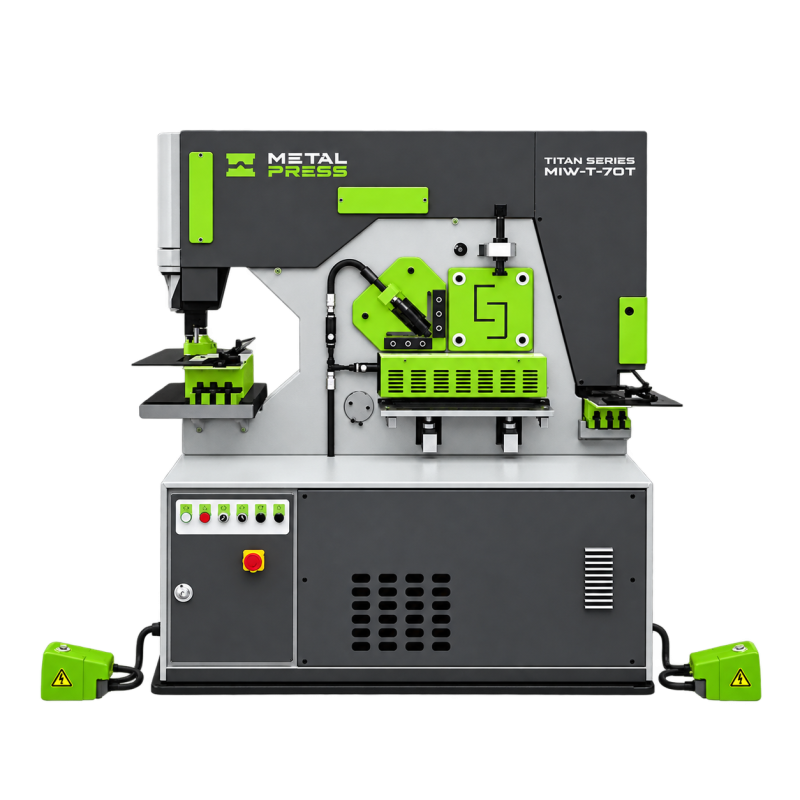
MIW-T Hydraulic Ironworker
Compare individual workstation ratings, throat access, models and optional tooling.
Notching prepares clearances and local profiles
The notching station removes a tool-defined portion of the workpiece. Specify notch width, depth, shape and position, together with access around angle legs or existing features. The required outline must fit the tool and machine geometry.
Use plate and angle punching and notching to organize these feature details. A triangular or complex contour may require a different cutting route rather than an assumed all-purpose notch tool.
Optional operations and complete-part routing
Some ironworkers accept bending or other special tooling, but those attachments are configuration-dependent. Their working length, force and access must be reviewed separately. They do not make the ironworker interchangeable with a full-length CNC press brake.
The MIW-T product page lists the MetalPress workstation families and optional tooling. For a finished mounting bracket, use bracket fabrication planning to coordinate the cuts, holes, notches and any separate bending operation. Confirm supplied tooling and operator arrangements in the quote.
A useful demonstration uses a representative part family rather than unrelated maximum-capacity samples. Ask how the same stock is cut, located, punched and transferred, including any operation that remains on a separate machine.
Continue planning your fabrication workflow
Frequently Asked Questions
What does an ironworker machine do?
It brings several dedicated fabrication operations together. The exact stations and optional attachments depend on the machine.
Is an ironworker a CNC punch press?
Not inherently. A multi-station ironworker and a dedicated production punch press have different machine and tooling arrangements.
Can one tonnage number describe every station?
No. Read each workstation’s capacity and tooling limits for the actual material and geometry.
Discuss the actual part and equipment configuration
Send the drawing, material specification, quantities and acceptance requirements to MetalPress Machinery. Confirm the final machine, tooling and operating requirements against the supplied documentation and application review.