
From Production to Installation: An MGS-08-4000 Guillotine Shear for an Ohio Automotive Manufacturer

An MGS-08-4000 hydraulic guillotine shear project for an Ohio automotive manufacturer, from production and pre-shipment preparation to shipment and installation.
An MIW-T-130 Hydraulic Ironworker for a Home-Appliance Manufacturer in Chicago
An MIW-T-130 hydraulic ironworker project for a Chicago home-appliance manufacturer, from application review and production to delivery and installation.
From Drawing to Shop Floor: A Titan Press Brake Project in Michigan
The conversation began with a set of part drawings. A Michigan manufacturer of industrial enclosures and equipment panels was planning its next CNC press brake around the work already moving through the shop: cabinet doors, folded panels and mounting brackets, each with its own bend sequence and locating requirements. In this illustrative project, that discussion led to a Titan MPT-SV-180T-8FT servo-hydraulic CNC press brake. The story follows the order from application review through factory inspection, delivery and installation.
Why a Perfect CAD Bend Becomes a Bad Part: The Science of Press Brake Springback
A bend can match its intended geometry under load and still miss the drawing after the tools release it. Press brake springback is the elastic recovery behind that change. The engineering task is to predict or measure the recovery, distinguish it from other errors, and validate the unloaded part. This briefing explains the physics, the limits of a springback calculation, and a practical way to build a repeatable compensation record. All numerical examples below are hypothetical calculations—not Titan test results or machine-setting instructions.
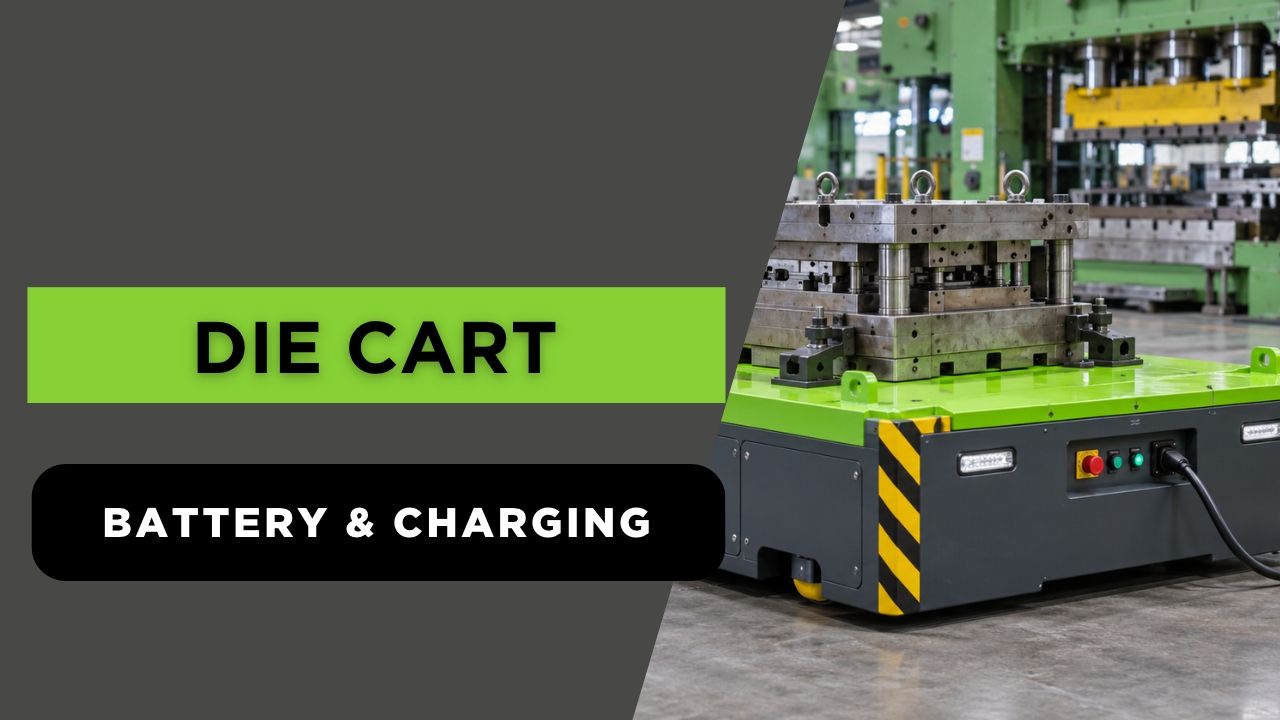
Die Cart Duty Cycle and Battery Charging for Multi-Shift Operation
Plan die-cart battery duty and charging windows from loaded trips, auxiliary demand, usable energy and the approved battery–charger combination.

Die Cart Floor Loading and Route Surveys for Heavy Tooling
Plan a heavy die-cart route using wheel reactions, floor conditions, clearances and handoff data—not payload capacity or average floor pressure alone.
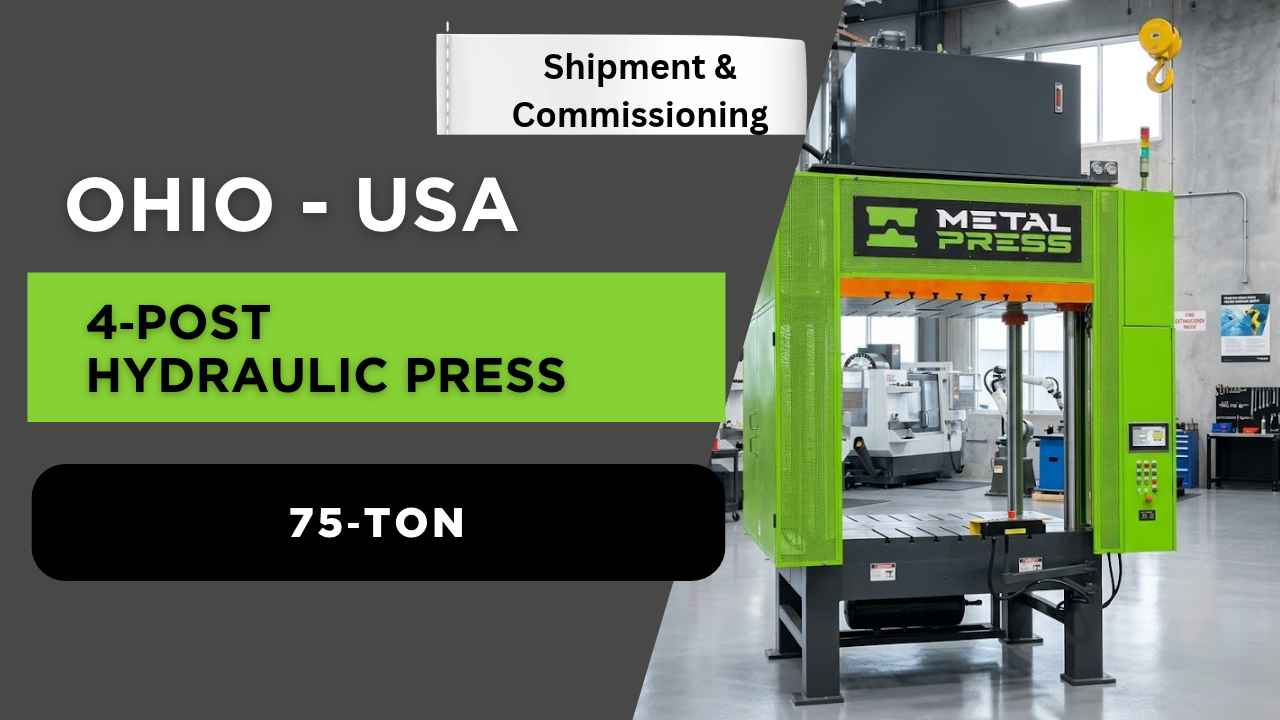
Shipping, Installation, and Commissioning the 75‑Ton 4‑Post Hydraulic Press in Ohio

Summary: This final phase of our project follows the journey of a custom‑engineered 75‑ton 4‑post hydraulic press as it leaves o...

75–150 Ton Hydraulic Presses: 100 Ton Press Machines for Industrial Applications
Hydraulic presses in the 75–150 ton range represent one of the most widely used force classes in industrial manufacturing. A 100 ton pr...
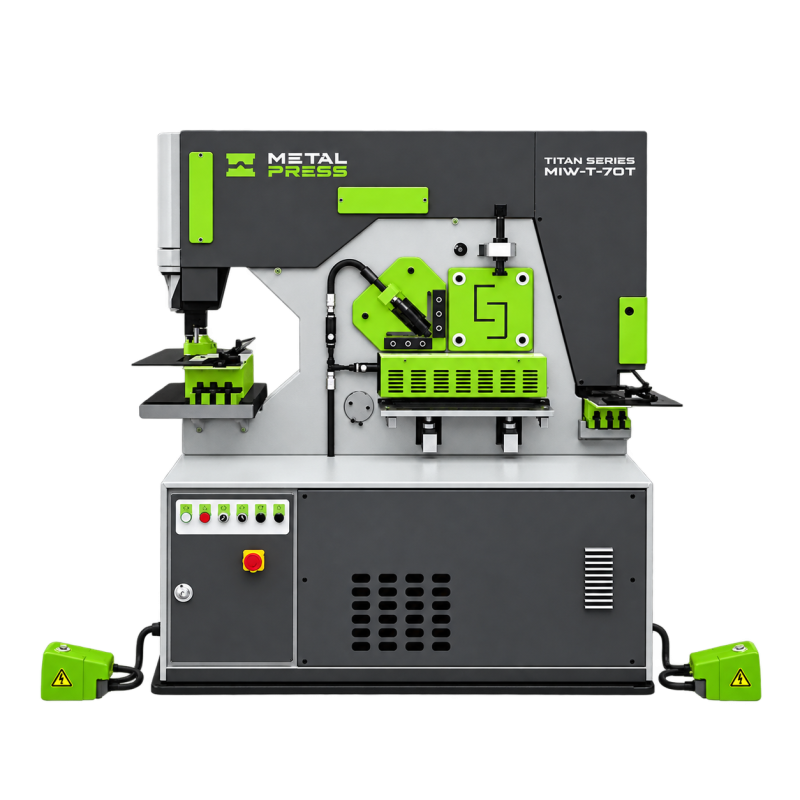
Ironworker vs Punch Press for Plate and Fabrication Work
An ironworker combines several fabrication stations, while a punch press is selected around a dedicated press-and-tooling production task. This briefing compares their roles for plates, brackets and repeated features. The useful choice comes from the part family, tooling investment, positioning method and production route—not a claim that either machine is always better.
Ironworker Punches, Dies and Hole-Punching Setup
A usable ironworker punching setup requires compatible punches, dies and holders, an approved material-and-hole combination, suitable access and a defined inspection method. This briefing organizes those decisions before tooling is ordered. It does not prescribe universal clearances or replace the machine and tooling supplier’s instructions.
What Is an Ironworker Machine? Five Fabrication Operations Explained
An ironworker machine combines dedicated metal-fabrication workstations such as punching, stock shearing and notching in one platform. It is equipment, not the ironworker trade or occupation. Its value is the ability to route suitable plate, bar and angle work through several operations, with each station selected by its own rating and tooling.
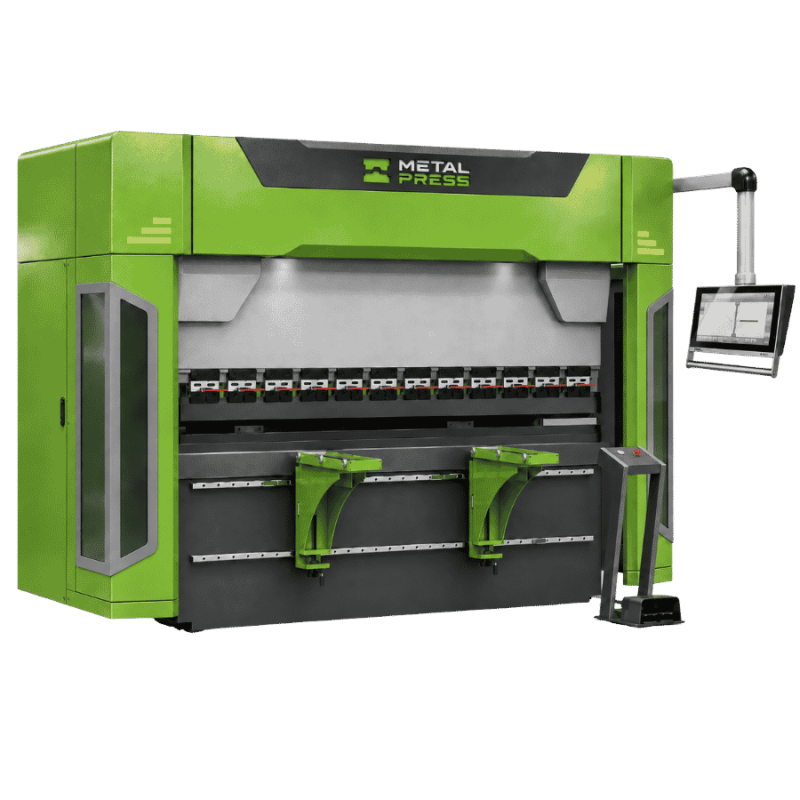
Press Brake Tooling and Bending Methods
Tooling selection connects the material and bend geometry to the press brake’s force, clearance and load limits. Air bending, bottoming and coining are distinct methods with different setup requirements. This briefing explains the decisions to review before selecting a punch, die and holder arrangement; it does not approve every method for every machine.
Press Brake Crowning and Bend-Angle Consistency
Press-brake crowning compensates for deflection along the bending system so the tooling relationship can be managed across the working length. It belongs in the setup and inspection plan for long bends. This briefing explains what crowning addresses, what it does not measure and how to specify a meaningful bend-consistency review.
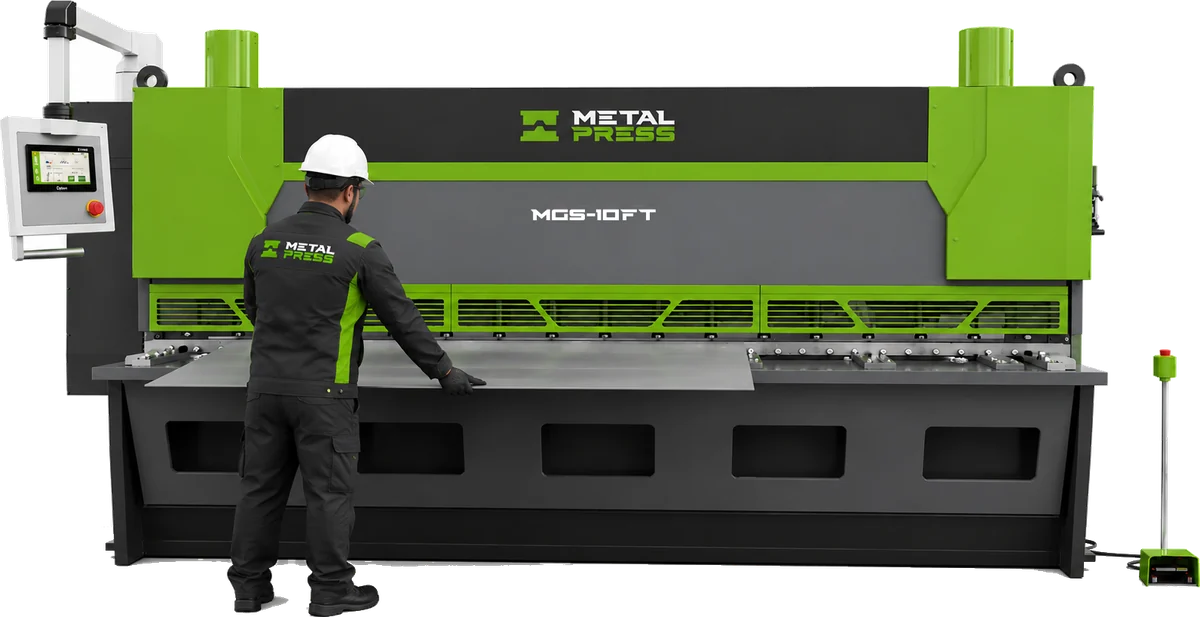
Guillotine vs Swing-Beam Shears: Architecture and Drive Choices
Guillotine and swing-beam terminology concerns the cutting mechanism, while hydraulic and mechanical terminology concerns its drive. Names are not used consistently across the industry, so a useful comparison starts with the actual blade-carrier motion, adjustment functions, capacity and support package. This briefing provides a specification checklist rather than a universal winner.
Press Brake Drives and Controls: Servo-Hydraulic, Hydraulic and Electric
Press-brake drive technology and CNC control describe different parts of the machine. Hydraulic, servo-hydraulic and electric identify aspects of force and motion generation; CNC describes programmed control. This briefing separates those terms so quotations can be compared around the workpiece, duty pattern and supplied configuration.
Shear Rake Angle and Blade Clearance: Burrs, Twist and Bow
Rake angle, blade clearance, blade condition and material support influence how a shear separates a blank and what edge or distortion remains. This briefing explains those variables as a system, with particular attention to narrow strips. It is a planning and inspection guide, not a universal adjustment recipe.
How to Choose a Hydraulic Guillotine Shear
Choose a guillotine shear from the actual material, full cutting length, required blank quality and sheet-handling sequence. Compare the thickness-and-width combination for the selected model, then review gauging, support and the narrowest strips. A thickness rating by itself is not a complete capacity specification.
How to Choose a Hydraulic Ironworker: Capacity, Throat Depth and Operators
Choose a hydraulic ironworker by comparing every required workstation with the actual stock and feature geometry. Punching force, hole size, throat reach, section capacities, tooling and operator arrangement must all fit the job; one tonnage figure cannot describe the whole machine.
How to Choose Press Brake Tonnage, Bending Length and Backgauge
Choose a press brake by checking the force required for the actual material and bending method, the longest bend, the tooling limits and the access needed through the complete bend sequence. Tonnage alone does not establish whether a machine can make the part.
How to Choose a Die Cart: Capacity, Height and Transfer Method
Choose a die cart or mold transfer cart by capacity, load center, deck height, route, transfer method, controls, safety, cost and ROI.