

Blog
100-Ton Powder Compaction Servo Press Shipment and Commissioning

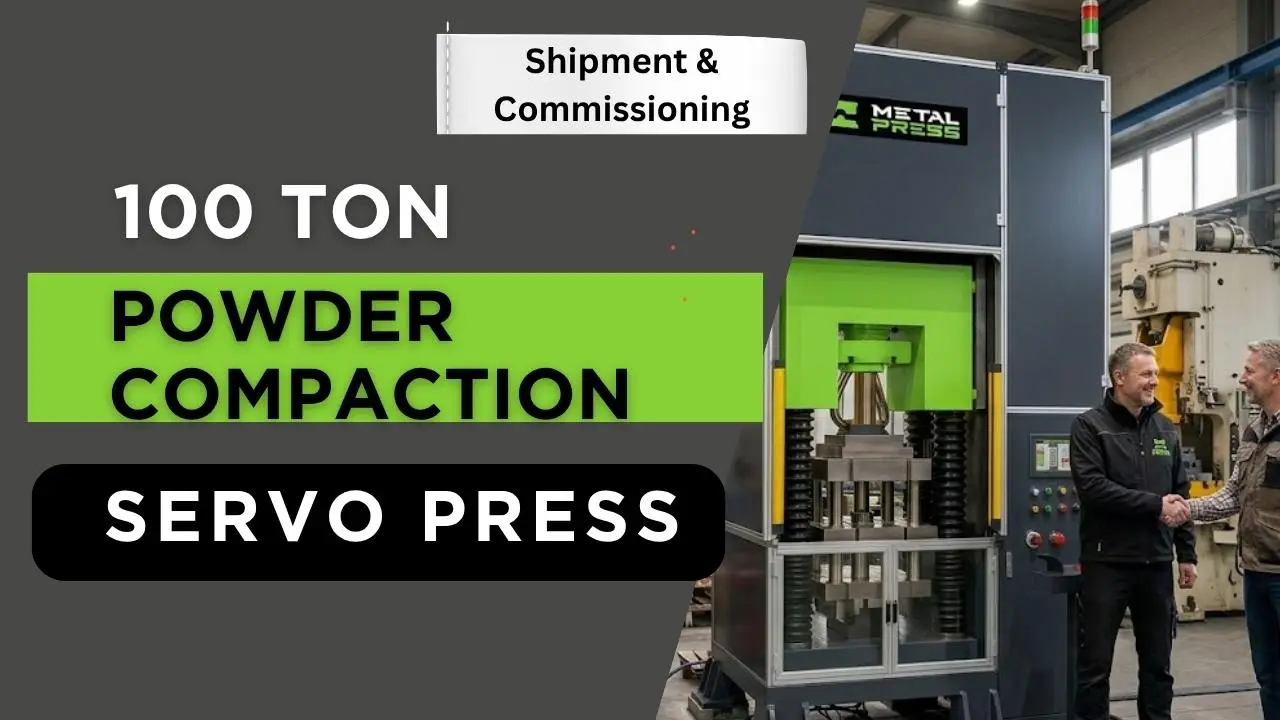
This 100-ton powder compaction servo hydraulic press (MPC-SV-100) project story follows shipment preparation, site installation and commissioning planning. The earlier design and assembly story covers the build, while the testing and finalization article explains the factory acceptance test (FAT) and inspection workflow.
Use the MPC-SV servo-hydraulic powder compaction press product page for current machine models, specifications and an equipment enquiry. The checklist below connects packaging, logistics, utilities, first-article verification and training to the agreed project scope; the signed records establish which activities and results apply to the delivered machine.
Review the earlier design and assembly, test and pre-commissioning stages of this MPC-SV-100 project.
Powder Compaction Servo Hydraulic Press
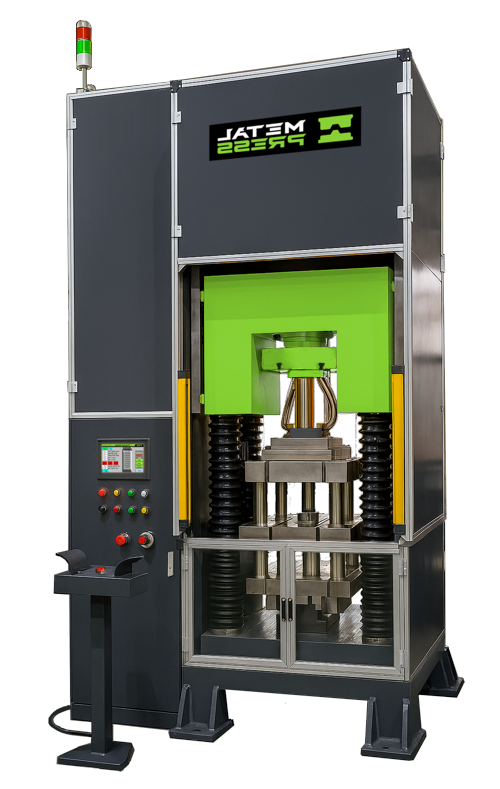
The MPC-SV powder compaction servo press uses servo-hydraulic drive technology for powder metallurgy and industrial forming applications. Define the required closed-loop force and position control, stroke lengths, customizable bed dimensions and single- or multi-station tooling configurations for the selected machine.
The current family has eight published model ratings from 44 to 660 US tons. Review the MPC-SV model table and configuration requirements for the corresponding metric ratings and working envelope. The article’s 100-ton project label is retained without assuming an exact conversion or an as-built force rating.
For equipment selection, specifications and a request for information, review the MPC-SV Series powder compaction press.
Shipment Preparation and Protective Packaging
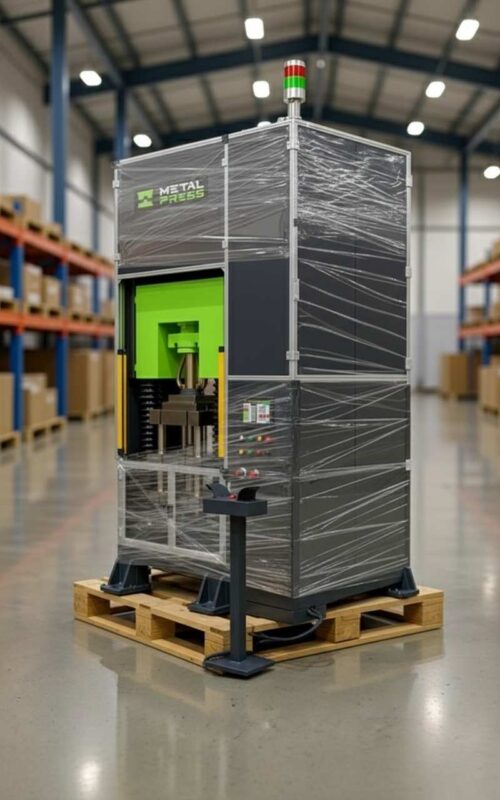
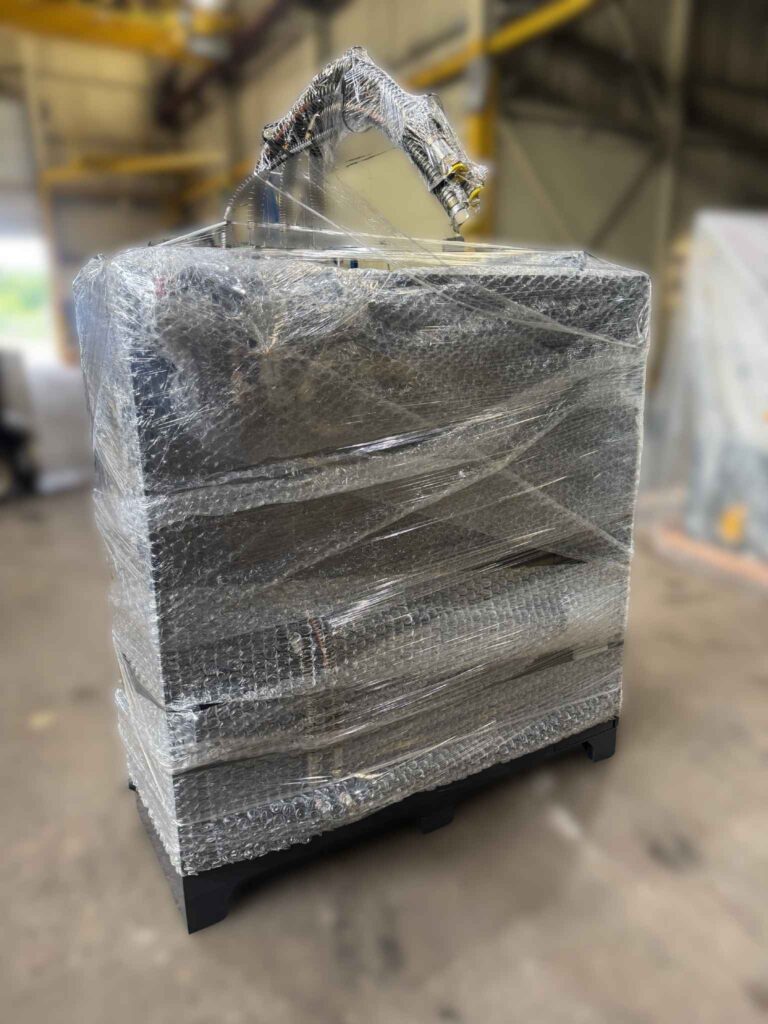
Shipment preparation for a high-precision powder compaction servo press brings together mechanical security, environmental protection and logistics traceability. Agree the packaging method with the supplier and carrier for the actual machine, route and handling conditions.
- Mechanical security: identify factory-approved shipping braces and internal tie-downs, secure moving components against ram or platen travel, and record critical fastener torque values in the torque log.
- Environmental protection: specify corrosion inhibitors, desiccant packs and protection for sensitive surfaces and electronics as appropriate. Hydraulic ports and filters need suitable closure and protection. Assess climate-controlled transport for climate-sensitive routes rather than assuming it is included.
- Crating and shock mitigation: confirm whether the shipment requires a wooden crate, vibration-rated packaging, engineered shock mounts or shock sensors. Record the approved crate design and photograph the packaged equipment for insurance and customs documentation.
- Labeling and service access: identify lifting points, service points and external panels. Supply the crate packing list and a photograph set for receiving inspection.
The packaging record supports damage inspection and helps preserve the factory baseline for on-site unpacking and installation. The supplied shipment documents should identify the measures actually used.
Logistics Coordination and Documentation
Logistics coordination aligns the heavy industrial equipment carrier, handling plan, shipping documentation and site readiness before dispatch.
- Shipping documentation: agree the shipping dossier, including the applicable FAT report, calibration certificates, HMI recipe exports, PLC program snapshot and commissioning checklist. Keep customer technical files available to the authorized project team; provide carriers and customs brokers with the documents relevant to transport and clearance.
- Carrier selection and routing: confirm handling responsibilities, routing, customs brokerage and pre-clearance documentation where required.
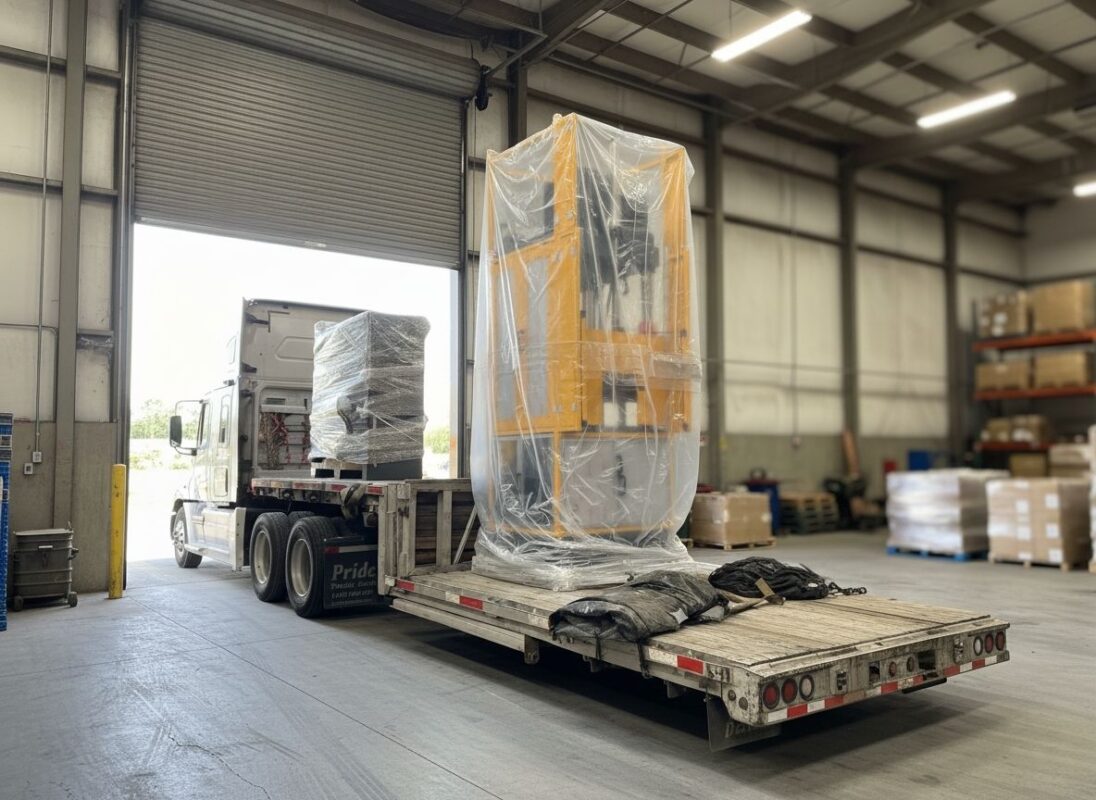
- Arrival windows and site readiness: review crane capacity, floor loading, dock access, local handling equipment and receiving space against the machine drawings. Assign the site-arrival checklist to named project contacts.
- Transit monitoring: if shock and tilt sensors are included, agree how their logs and the transit monitoring report will be reviewed and how anomalies will be handled before on-site commissioning.
Complete documentation helps the receiving and commissioning teams identify outstanding issues before installation proceeds. Delivery windows and commissioning dates remain project-specific.
On‑site Commissioning and Final Installation
On-site commissioning connects the delivered press to the approved utilities, tooling and operating procedures in preparation for pilot production. Agree the installation and handover program, responsibilities and acceptance criteria before the machine arrives. The powder press testing and inspection story provides context for the factory baseline to be reviewed on site.
Site arrival and unpacking
- Inspection and sign-off: inspect the crate and machine against the packing list, photograph their condition and review shock sensor logs if included. Document transit damage and resolve installation hold points.
- Positioning and leveling: use the approved lifting plan and suitable site crane or handling equipment. Record leveling readings and anchor bolt torque values against the installation instructions.
- Utility hookups: verify electrical supply, cooling water and any specified hydraulic or pneumatic connections against the machine requirements. Complete grounding and electrical safety checks before energizing the equipment.
System integration and verification
- HMI and PLC transfer: verify the approved HMI recipes, PLC program snapshot and configuration backup. Control and document any transfer or change to the on-site controller.
- Sensor and safety checks: review the installed load cells, position transducers, thermocouples and safety interlocks as applicable to the supplied configuration. Qualified personnel should verify light curtains and emergency stops using the approved commissioning and safeguarding procedures.
- Dry runs and mechanical checks: confirm motion profiles, limit switches, mechanical clearances and lubrication points through the approved no-powder dry-run sequence. Check robot handshakes where an automation interface is included.
First‑article verification and pilot readiness
- Warm-up and thermal stabilization: use the agreed warm-up protocol and monitor oil temperature and hydraulic pressures against the acceptance plan before comparing measurements.
- Verification run: define the sample size, customer’s tooling, powder lot and measurement method with the customer’s quality engineer. Compare the on-site results to the applicable FAT report and investigate differences in setup or conditions. A fixed part count does not suit every acceptance plan.
- Recipe tuning: document changes to HMI recipes and their effect on the verification run, including changes associated with site conditions or powder lot variation.
First-article verification and pilot readiness should be recorded against the agreed acceptance criteria, rather than inferred from installation alone.
Operator Training and Documentation Handover
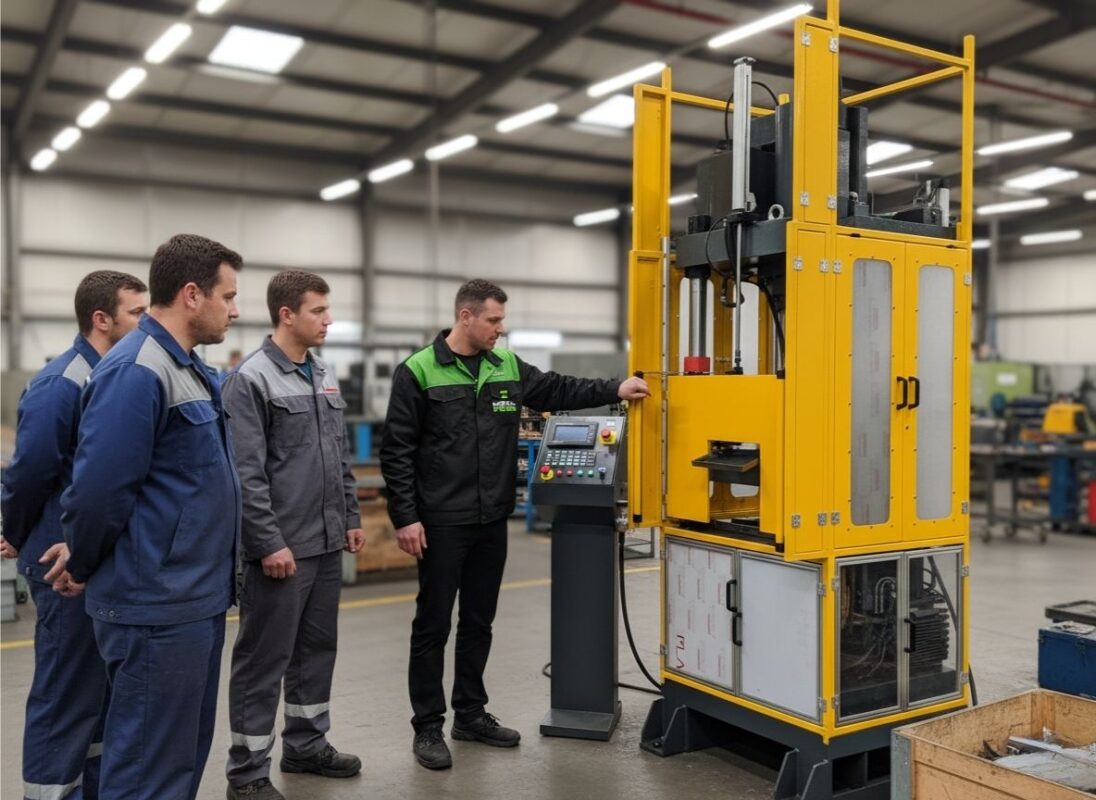
Operator training and documentation handover prepare the customer’s team to use and maintain the supplied configuration. Agree the training scope and document the responsibilities of operators, maintenance personnel and the project team.
- Hands-on operator training: cover HMI recipe selection, startup and shutdown, routine checks, basic troubleshooting and repeatable setup steps. Review force vs. displacement overlays where that data is available.
- Maintenance and service training: review lubrication schedules, hydraulic filter changes, sensor recalibration procedures, mechanical inspection points, torque values, spare parts lists and preventive maintenance intervals.
- Documentation package: identify the applicable operation and maintenance manuals, commissioning checklist, FAT report, calibration certificates and HMI recipe exports. Agree controlled delivery and backup of the documents.
- Knowledge transfer session: review data interpretation and the agreed repeatability protocol. If capability indices (Cp/Cpk) are required, define the measurement system, sample plan and process conditions before interpreting them.
The handover record should identify completed training, outstanding actions and the escalation path for technical support.
Post‑Commissioning Support and Early Performance Monitoring
Post-commissioning support helps the customer review early production and the ramp to volume. Include support responsibilities, access arrangements and response expectations in the project agreement.
- Remote support and telemetry: where enabled and authorized, review cycle logs, alarms and key process variables with the support team. Confirm the available remote telemetry and logging scope.
- Follow-up visits: agree whether follow-up visits or remote reviews are included, with timing based on the production plan rather than an assumed first-week commitment.
- Warranty and spare parts: review the actual warranty terms, recommended spare parts and ordering procedures for the selected configuration.
- Performance review and ROI tracking: define KPI dashboards for scrap rate, cycle time, green density σ and setup time where relevant. Use measured production data and a consistent baseline to assess yield improvements and the ROI case.
Report the observed performance and unresolved actions separately. Project-specific results, rather than a general promise, establish the value achieved.
Planning Your Powder Press Shipment and Commissioning
Shipment and commissioning link factory validation to the customer’s production process. Agree packaging, logistics, installation, first-article verification, operator training and support before dispatch, with signed records for the supplied machine.
For equipment selection, start with the MPC-SV powder compaction press. Use the powder metallurgy press machine guide and powder pressing application hub to prepare the powder, tooling and process requirements.
If you are planning a pilot or need a commissioning quote, discuss your powder press installation and commissioning requirements. Provide the machine configuration, site layout, utilities, tooling, powder information and target production plan so the timeline, resource list and documentation scope can be reviewed.
Contact MetalPress engineers and specialists to review the project scope.
Let Us Make Your Next Powder Compaction Press
Whether you are in the USA, Canada, Mexico or South America, contact MetalPress for powder-compaction information, a quote and consultation. Include the required capacity, part drawing, powder details, tooling concept and installation conditions.
Visit all our products